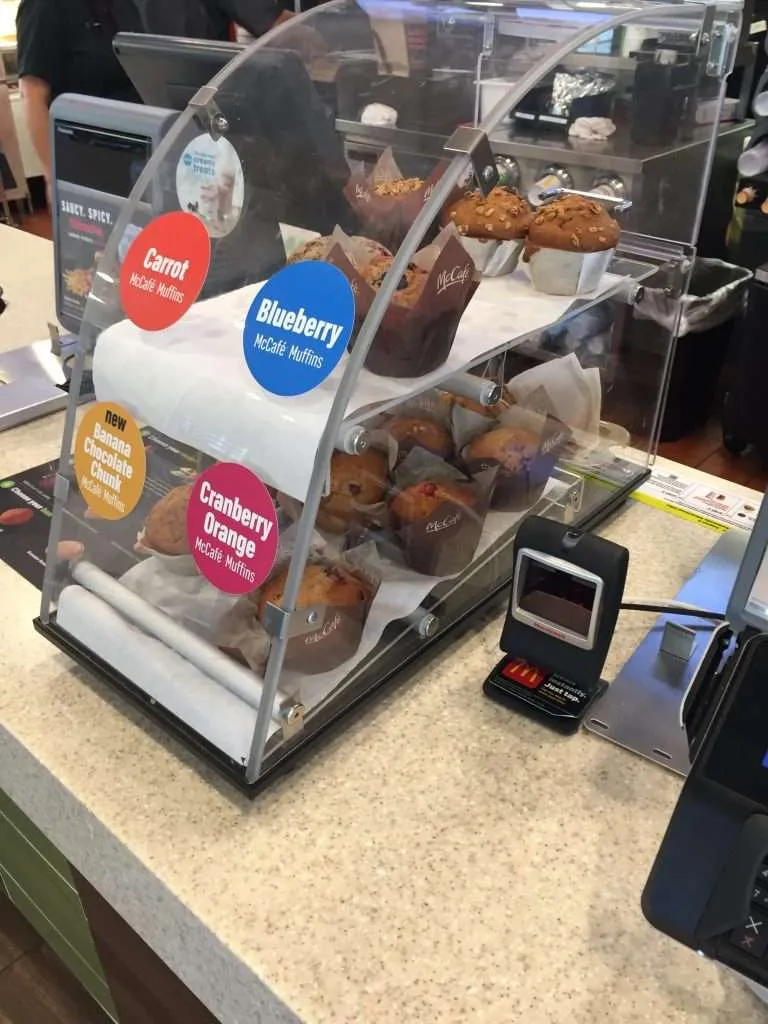
Pick up a clear brochure holder, an easel-back sign, a J-hook, a folded sign base — nearly every acrylic part with a fold in it was made the same way, by the most common forming operation in display fabrication and the least explained one online. It is called line bending, it is beautifully simple in principle, and its design implications are where folded parts go right or wrong. Here is both halves.
The process itself
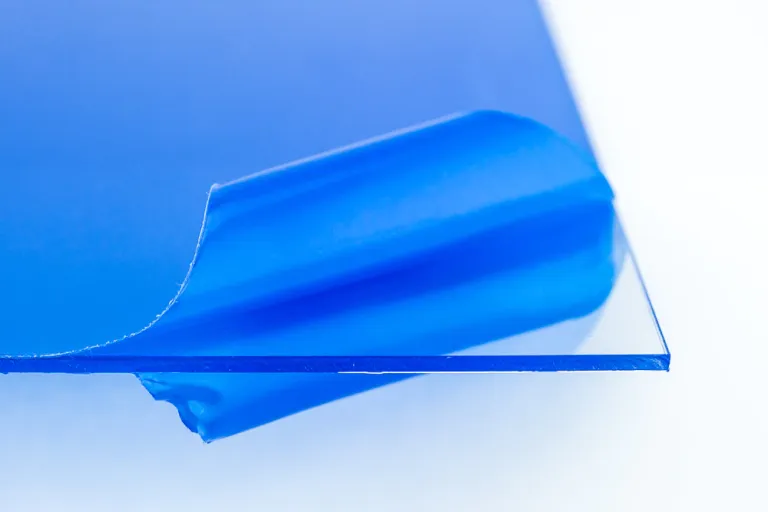
A strip heater — a narrow heating element the width of the sheet — softens a thin zone across the acrylic along the intended fold line, leaving the rest of the sheet rigid and cool. When the zone reaches forming temperature, the part is folded along that line against a stop or fixture that sets the angle, and held there while the material cools and the fold sets. That’s the whole operation: a controlled local softening, a controlled fold, a controlled hold. Its elegance is that only the bend line is ever formed — the flats stay flat, printed graphics away from the line stay undisturbed, and the finished part keeps sheet-flat faces joined by clean radiused folds.
Heat management is where craft lives
The variables the operator controls — which side is heated, how long the material dwells on the heater, how wide the softened zone runs — scale with material thickness, and they are set per material and thickness rather than guessed. The failure mode they guard against is visible: a fold made with the heat wrong for the thickness stresses the outside face of the bend, which can read as whitening along the line — the material telling you its outer skin was stretched before it was ready. Thicker sheet in particular is heated from both sides so the softened zone develops through the full thickness instead of only at the surface. For the designer, none of this is homework to do — it is why “just put a fold there” is a fabrication operation with parameters, not a default that comes free.
Bend radius follows thickness
A line-bent fold is not a sharp crease; it is a radius, and by default the inside radius of a fold comes out on the order of the material’s thickness. That is a design input, not a machine setting. Pushing for a visibly sharper fold concentrates stress at the bend and invites whitening; designing with the natural radius gives a clean, strong fold that looks intentional. If the design genuinely needs a crisp square corner, that is usually a signal the part wants different construction at that feature — bonded construction makes square outside corners, folding makes radiused ones, and plenty of good parts combine both.
Bend sequence is engineering
On a part with one fold, order is trivial. On a part with several, order is design: each fold changes the part’s shape, and a later fold needs clear access for the heater and room for the already-folded geometry to clear the machine. A five-bend part that folds beautifully in one sequence may be physically impossible in another — a wall folded too early can block the heater from reaching the next line. This is why a multi-bend part’s design review includes a folding-order check, and why unusual folded geometries are worth a conversation before the drawing locks: the shop is checking not just whether each fold is makeable, but whether they are makeable in some order.
Accuracy expectations: formed ranges, not machined ones
A folded part’s legs and angles are set by heated forming, and they hold formed-range tolerances — per the Acrylic Fabrication Tolerances standard, thermoformed components run approximately ±3% to ±5% of the formed dimension, a fundamentally different band than the cut edges of the same part, which hold their cutting process’s range. The design move that follows is simple: put the critical dimension on the leg that matters functionally, dimension it from the fold, and let the standard govern the rest of the formed geometry. A folded part dimensioned as if every leg were machined is a drawing asking for precision the process doesn’t sell — and usually doesn’t need.
Folded parts are everywhere in retail and POP work because the operation is fast, clean, and economical — a single fold replaces a bonded joint, a fastener, or a second part. If your design has folds in it, send the drawing with thickness and the critical legs flagged, and the folding-order review comes back with the quote.