Most custom fabrication is planned around what the thing needs to be. Exhibit fabrication is planned around when the thing must exist. A trade show date is set by an organization you have no relationship with, published to an industry, and attached to a hall that will open its doors whether your booth is in it or not. Nothing else in commercial fabrication has a deadline with that shape: not negotiable, not internal, and enforced by an empty ten-by-twenty where your product line was supposed to be.
That one fact organizes everything in this guide. The material choices, the construction decisions, the production tier, the freight mode — each is downstream of an immovable date, which means each is really a scheduling decision wearing a different costume. Plan them in that spirit and a show build is a controlled process. Plan them as if the date were soft and the build will teach you, expensively, that it was not.
What actually gets fabricated for a booth
“Exhibit” usually means the whole environment — structure, graphics, AV, flooring — but the fabricated acrylic and plastic scope inside it is a specific list, and each item on it maps to a fabrication process:
- Product demo fixtures. The stands, cradles, risers and holders that put the product at hand height and eye line. Typically CNC- or laser-cut, bonded, and finished to the grade the viewing distance demands — these are the parts attendees stand closest to.
- Counters, podiums and lead stations. Larger bonded assemblies, often combining acrylic with other materials as the design requires. Structural bonding and edge finishing dominate the work.
- Lit and printed panels. Edge-lit or back-lit acrylic carrying UV-printed brand graphics — the cutting is straightforward; the color management and the proof cycle are where the schedule lives.
- Literature and lead-capture pieces. Brochure holders, card drops, giveaway trays. Small, often ordered in quantity, and the classic thing that gets remembered two weeks before move-in.
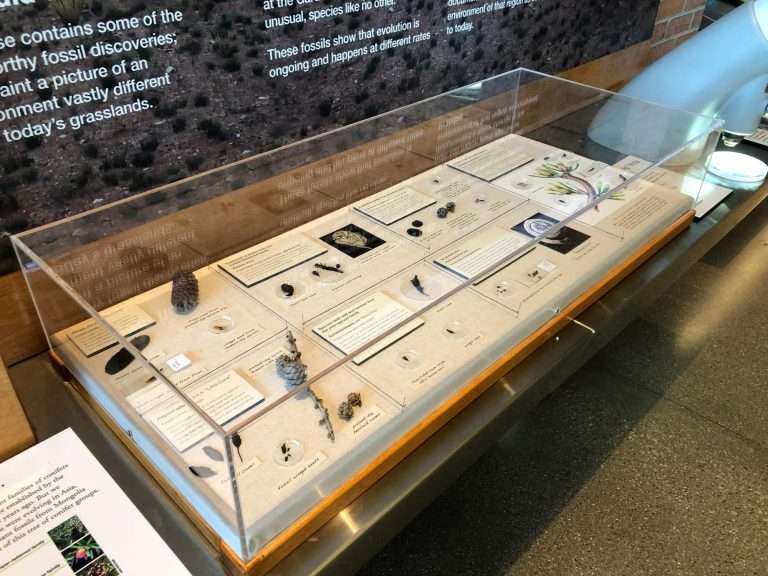
- Cases and vitrines for hero product. Bonded clear enclosures protecting the thing the booth exists to show. These carry the tightest finish expectations in the booth, because attendees put their faces against them.
- Thermoformed elements. Curved faces, domes, and formed trays where flat stock can’t make the shape.
The reason to think in this component map early: the items have different production characters. Printed panels wait on artwork and proofs; bonded casework wants finishing time; quantity pieces want their run scheduled as a run. A booth is not one job — it is a small portfolio of jobs sharing a deadline.
Materials for the exhibit life cycle
An exhibit part has a harder life than almost any other fabricated display. A retail fixture ships once and stands still; an exhibit part is crated, trucked, forklifted across a marshaling yard, uncrated by whoever is on the install crew, stood up for three days, and then does the whole trip in reverse — per show, for as many shows as the program runs. Materials should be chosen for that life cycle, not for opening night alone.
The honest division of labor:
- Acrylic where clarity and finish present the brand. Demo fixtures, vitrines, lit panels, and anything judged at close range. Acrylic takes a polished edge and a defined finish grade in a way that presents product properly, and its optical clarity is the reason clear display work defaults to it.
- Polycarbonate where the road will punish the part. The crate-truck-drayage-teardown cycle finds brittle details. For parts that get handled hard — panels that flex during install, pieces near the crate’s impact zones, components an install crew will lever against — polycarbonate’s impact behavior buys survival. The trade is real: it scratches more readily than acrylic and doesn’t take the same polished edge, so it earns its place on the parts that get handled, not the parts that get looked at.
Two practical corollaries. First, thickness and construction should reflect handling loads, not just standing loads — the part’s worst day is in transit. Second, a spec that names its finish expectations in measurable terms travels better across seasons and reorders: a demo fixture specified to Display Finish, judged at approximately 2 feet, with named edge treatments from the edge finishing classifications, can be rebuilt to match years later. “Like the last one, but nicer” cannot.
The timeline counts backward from move-in — not the show date
The date printed on the show’s website is not the date that governs fabrication. The governing date is the one at the bottom of a chain that starts weeks earlier:
- Advance-warehouse window. Most shows offer (and effectively expect) freight to arrive at an advance warehouse in a window that opens roughly a month before the show and closes days before move-in. Miss it and you are into direct-to-show-site delivery with tighter targeting and less forgiveness.
- Freight transit. Working days, not calendar days, and dependent on mode and distance. This is a number your freight partner commits to — get it in writing per show.
- Crating and pack-out. Custom crates for custom parts are their own small fabrication job. They cannot start until final dimensions exist and should not finish the night the truck arrives.
- Production span. The fabrication itself — which cannot begin until the last approval lands.
- Proof approval and design lock. Printed graphics wait on proofs; production waits on sign-off. Every day an approval sits in someone’s inbox is a day removed from production, and the deadline absorbs none of it.
Build that chain for a real show and the order date lands far earlier than intuition suggests — months ahead of the show itself. The chain is also where scheduling language has to get precise, so here is the precise version, exactly as our Production Scheduling standard defines the three service levels: Production Schedule work is scheduled by available fabrication and assembly capacity and completed in sequence with other scheduled work — no guaranteed ship date. Accelerated Production moves a project forward in the schedule when available capacity allows — improved timing, but also not a guaranteed ship date. Reserved Production allocates dedicated fabrication capacity to guarantee a specific ship date.
An exhibit deadline is Reserved Production’s textbook case — it is on the standard’s own list of what the tier exists for. When the chain above has no slack in it, the fabrication link should be the one link that is guaranteed, and only one tier guarantees it. When a program does carry slack — an exhibit fleet refreshed between shows, spares built in the off-season — the other tiers fit that flexibility. The mistake is not choosing a lower tier; it is choosing one without noticing which kind of date your show math actually requires.
Logistics is a design input, not a shipping detail
The biggest exhibit-cost surprises happen after fabrication, and most of them were designed in months earlier:
- Crate-ability. A part that breaks down into flat, stackable elements crates small; a bonded monolith crates as its own volume plus protection. Designing the split points — what bonds in the shop, what assembles on the floor — is a decision about freight and drayage as much as structure.
- Weight. Drayage — the move from the loading dock to your booth space — is billed by weight. That makes every pound a recurring cost paid again at every show, and it is a cost factor you design down (thinner where structure allows, aluminum or honeycomb substrates behind acrylic faces, hollow construction) rather than negotiate down.
- Damage-prone details. Unsupported corners, proud edges, thin projecting tabs, and hardware that protrudes past the part’s plane are where teardown damage concentrates. A detail that survives the showroom can still lose a fight with a forklift; edges that take impact deserve protection or radiusing at design time.
- Spares strategy. For a program with real dates riding on it, the cheapest insurance is fabricated at the same time as the primary: a spare demo fixture, a second set of the small parts that walk away, replacement hardware. A spare made during the run is marginal work; the same part made alone, two days before a show, is a schedule crisis.
Program thinking beats project thinking
A brand doing four shows a year does not own a booth — it owns an exhibit fleet, and fleets reward management. The parts have refresh cycles (graphics change faster than structures), wear points (whatever touches the crate), and a natural reorder rhythm. Handled as a program, each next show is an order against files on record — dimensions, finish grades, print artwork, crate drawings all already agreed — rather than a rebuild from scratch. That is when the earlier discipline pays off twice: the measurable spec that made the first build inspectable is the same document that makes the fifth build identical to it.
It also changes the scheduling conversation. A program with a show calendar can put its predictable work into the standard production flow through the year and reserve capacity only where a hard date demands it — which is a calmer, less expensive way to run an exhibit fleet than treating every show as an emergency.
Where to go deeper
This guide is the map; the specifics each deserve their own working session. For the backward-planning math on a real deadline, the scheduling tiers in full, and the fit-up tolerances that make multi-part booths assemble on the floor, start with the Production Scheduling standard and the Fabrication Tolerances standard — and when the show calendar already has a date on it, bring it to us early: the more calendar that exists between the conversation and move-in, the more options exist for everything else in this guide.