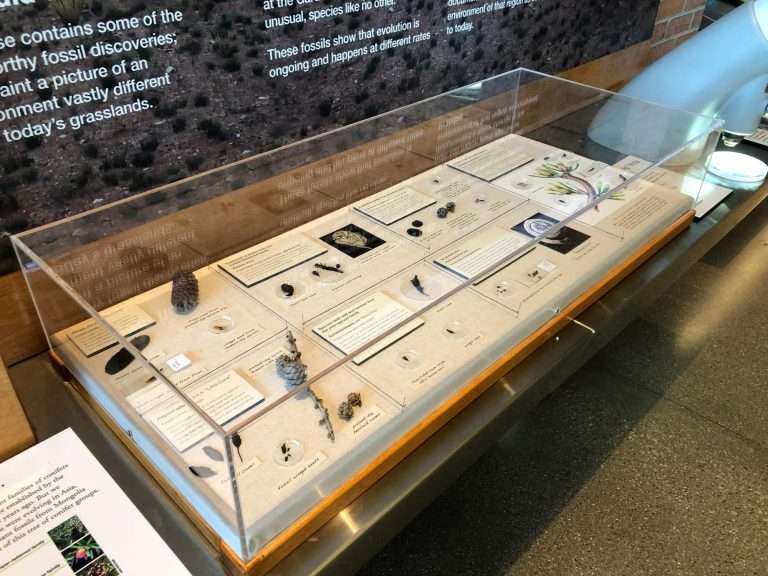
Nearly every vitrine acceptance dispute in this industry traces back to the same sentence in the spec — the one that says the case shall be “seamless” or “crystal clear.” Those words feel rigorous when the drawing goes out. They stop meaning anything the moment a case arrives and two professionals disagree about whether it complies, because neither word comes with an inspection procedure. Seamless at what distance? Clear compared to what?
The fix is not more adjectives. It is a spec written in terms that can be checked: a named quality grade with a stated inspection distance, an edge-finish classification assigned to each visible edge, a joint-clarity grade, and tolerance bands drawn from a published table. This guide walks the anatomy of that spec field by field, gives you a template you can paste into a drawing note or RFQ, and covers the equally important question of what to leave out.
Why adjectives fail as acceptance criteria
A specification does two jobs. Before fabrication, it tells the shop what to build. After delivery, it tells the registrar what to check. The industry’s usual unmeasurable adjectives fail at the second job completely: there is no way to inspect a case against “flawless,” so acceptance becomes a negotiation between whoever unpacked the crate and whoever built the case — with both parties acting in good faith against targets that were never the same.
Measurable vocabulary closes that gap. The Akrylix quality standards define surface-quality grades by Inspection Distance — the viewing distance at which the piece is evaluated. Production Finish is inspected at approximately 4 feet, Display Finish at approximately 2 feet, and Museum Archival Finish at approximately 1 foot. A spec that says “Museum Archival Finish, inspected at approximately 1 foot” has replaced an argument with a procedure: stand at the distance, look at the surface, done. The same logic extends to edges, joints, and dimensions, and the rest of this guide applies it to each.
The anatomy of a vitrine specification
A complete vitrine spec covers eight things. Most specs we receive cover three or four of them and leave the rest to be discovered during the quote conversation — which works, but slower, and the discovered items never make it back into the acceptance criteria.
1. Dimensions and tolerance bands
State overall dimensions and interior clear dimensions, and know which one governs. A vitrine sized to cover a mount or fit a recess is governed by interior clearance; one sized to align with casework around it is governed by overall envelope. The wall thickness of the acrylic sits between the two, so specifying both without a governing note can produce a case that satisfies neither.
Then attach a tolerance band rather than a bare number. Per the published fabrication tolerances table, fabricated assemblies typically hold approximately ±1/16" to ±1/8". Cite that band for the general envelope, and separately flag any critical-fit dimension — a deck rabbet, a keyed base interface — where you need the tight end of it. Naming the one dimension that matters gets you exactly what you need; asking for tight tolerance everywhere just adds cost on the dimensions that do not.
2. Material and thickness
State the material — and if your institution’s practice calls for cast acrylic specifically, say so; a material preference stated in the spec is honored where practical. Thickness is different: it is driven by span. A wide unsupported top panel needs more thickness than the same footprint at half the width, and thickness selection for large spans is its own engineering decision, one we treat separately from spec writing. For spec purposes you have two sound options: state the spans and let the fabricator propose thickness at quote, or state a thickness and ask the fabricator to confirm it against the geometry. Either works. Silently assuming a thickness and discovering the deflection later does not.
Note that sheet thickness itself carries a tolerance of approximately ±10% of nominal, per the published table — worth remembering anywhere a thickness stacks into a fit.
3. Joint construction and Joint Clarity grade
This is the field the adjective “seamless” was always reaching for. Instead of the adjective, call out a grade from the Joint Clarity standards, which define what a bonded acrylic joint is permitted to look like at each grade level. The grade is the acceptance criterion; the bonding method that achieves it belongs to the fabricator (more on that below). One grade callout for the case is usually right — if a concealed base joint can live at a lower grade than the display joints, say so explicitly and save the labor for the joints a visitor will see.
4. Edge finish, per visible edge
Edges are where “specify per edge” earns its keep, because a vitrine’s edges do very different jobs. The edge finishing classifications name six finishes — Raw/Saw-Cut, Sanded, Laser-Cut, Flame-Polished, Buff-Polished, and Diamond-Polished — and the published guidance maps them to the quality grades: Production Finish work commonly carries flame-polished or sanded edges, Display Finish commonly buff-polished, and Museum Archival work is often diamond-polished. A sound vitrine spec might call for Diamond-Polished on the exposed top rim, edges within joints finished per the Joint Clarity grade, and Sanded on the concealed bottom edge that sits in a base channel. Three callouts, each matched to what the edge actually does.
5. Surface quality at a stated Inspection Distance
Name the grade and repeat its inspection distance in the spec, so the acceptance procedure travels with the document: “Museum Archival Finish, inspected at approximately 1 foot.” For collection display this is the usual grade; a case for a lobby installation viewed from walking distance may be honestly served by Display Finish at approximately 2 feet, and the spec that says so is making a deliberate, defensible choice rather than defaulting upward.
6. UV-filtering requirement
If the collection’s lighting policy requires UV-filtering acrylic, the spec must say so — it is a property of the sheet itself, not a finishing step. State the requirement as your conservation team defines it. If it is not required, saying so explicitly is also useful; silence forces the fabricator to ask.
7. Base interface and access method
How does the case open? Lift-off hood, hinged panel, keyed and locked deck — each drives different fabrication and hardware, and each implies who lifts what during object rotation. State the method and the interface geometry (channel, rabbet, cleat, or flush-set), and flag the interface dimension as critical-fit per field 1. If handling constraints limit the weight or size a preparator can lift, that constraint belongs in the spec too.
8. Sealing and ventilation, as your conservators require
Whether a case should be sealed, gasketed, or deliberately vented is a conservation decision that belongs to the institution’s conservators, based on the collection and its environment. The spec’s job is to record their requirement precisely so the fabricator can build to it — not to leave it as an open question the shop must guess at. Write down what the conservators specified, in their terms, and we build exactly that.
The template
The block below assembles the eight fields into a specification you can paste into a drawing note or RFQ and fill in. Bracketed items are project-specific; everything else is written in the published standards vocabulary and cites the published tolerance bands, so the spec and the acceptance criteria are the same text.
ACRYLIC VITRINE — FABRICATION SPECIFICATION
1. DIMENSIONS
   Overall envelope (W x D x H): [dimension] x [dimension] x [dimension]
   Interior clear (W x D x H):   [dimension] x [dimension] x [dimension]
   Governing dimension set: [interior clear / overall envelope]
   General tolerance, fabricated assembly: approx. +/-1/16" to +/-1/8"
     per the Akrylix fabrication tolerances table
   Critical-fit dimension(s): [dimension + location, e.g. base interface];
     hold to the tight end of the band; confirm at quote
2. MATERIAL
   Acrylic; [cast, if required by institutional practice]
   Thickness: [state thickness for fabricator confirmation, OR state
     spans and request thickness proposal at quote]
   Note: sheet thickness tolerance approx. +/-10% of nominal
3. JOINTS
   Construction: bonded; method at fabricator's discretion
   Joint Clarity grade: [grade] per the Akrylix Acrylic Joint Clarity
     Standards (display joints); [grade or "same"] at concealed joints
4. EDGE FINISH (per visible edge, per the Akrylix Edge Finishing
   classifications)
   Exposed top rim:        [Diamond-Polished / Buff-Polished]
   Edges within joints:    finished per Joint Clarity grade above
   Concealed base edges:   [Sanded acceptable / specify]
5. SURFACE QUALITY
   Grade: [Museum Archival Finish, inspected at approx. 1 foot /
     Display Finish, approx. 2 feet / Production Finish, approx. 4 feet]
6. UV FILTERING
   [Required — per conservation requirement: state it / Not required]
7. BASE INTERFACE AND ACCESS
   Access method: [lift-off / hinged / keyed-and-locked]
   Interface geometry: [channel / rabbet / cleat / flush-set]
   Handling constraints: [max lift weight or crew size, if any]
8. SEALING / VENTILATION
   [Record the conservators' requirement verbatim]
9. ACCEPTANCE
   Acceptance on delivery is inspection against sections 1-8 of this
   specification: dimensions within the stated bands, joints at the
   stated Joint Clarity grade, edges at the stated classifications,
   surface at the stated grade and Inspection Distance.
What to leave out
A spec gets stronger by omitting three categories of content, and each omission has a reason.
Process prescriptions. Bonding method, polishing sequence, cutting process — these are the fabricator’s to choose, because the fabricator owns the outcome. Specify “Joint Clarity grade X” and the shop selects the joint prep and bonding approach that achieves it; prescribe the bonding method and you have taken ownership of the result while giving up the shop’s judgment. The same holds for cutting: laser-cut edges are glossy but carry a slight taper that grows with thickness and suit thinner stock best, which is exactly the kind of process trade-off the shop should be free to make against your named edge classification rather than have dictated to it.
Over-tight tolerances on non-fit dimensions. The published bands exist because they describe what fabrication processes actually hold. Demanding tighter-than-band tolerance on the overall height of a case that fits nothing does not produce a better case; it produces cost and quote friction on a dimension nobody will ever measure with that precision. Reserve tight callouts for the interfaces identified in field 1.
Adjectives. If a word in the draft spec cannot be inspected — no distance, no grade, no band — it is a wish, not a requirement, and it will do its damage at acceptance time. Strike it, find the field it was reaching for, and write the measurable version.
Acceptance on delivery: the spec is the checklist
The quiet payoff of a spec written this way is that the receiving inspection already exists — it is section 9 of the template, pointing back at sections 1 through 8. The person unpacking the case checks dimensions against the stated bands, views the surface at the stated Inspection Distance, and checks joints and edges against the stated grades. No judgment calls about what a word meant; the document that ordered the case is the document that accepts it. (What a registrar should ask a prospective fabricator before any of this — about quoting, insurance, crating, and schedule — is a separate conversation we address on its own.)
One schedule note belongs in that pre-award conversation rather than the spec itself: if the case must be on the floor for a fixed opening date, only Reserved Production guarantees a ship date, and that is a scheduling-tier decision to settle at quote time, not a line to bury in a drawing note.
Specs meet fabrication
We fabricate to specifications written exactly this way, and the vocabulary above is our own published standards system — which is why a spec built on it needs no translation when it reaches our shop. Vitrines and display cases built in this shop have gone to the Whitney Museum of American Art, the Herbert F. Johnson Museum of Art at Cornell University, and the Everhart Museum, and the project gallery shows the kind of work those specifications produce.
If you have a draft spec — or a case to specify and a blank page — send it over. PDF is preferred for drawings, DXF/DWG accepted, and we will flag anything in the spec that needs a decision before it becomes a quote.