Steel tanks hold liquid better than acrylic ever will, and every research group that orders an acrylic tank knows it. They order acrylic because the walls are part of the instrument: the experiment is watching what happens inside — an animal behaving, a dye filament tracing flow, a sensor under calibration — and a tank you cannot see through is a tank that defeats the study. That inversion, transparency as the functional requirement, shapes everything about how research tanks are fabricated. Here is what that work actually involves.
The research tank menu
- Observation and behavior tanks — housing for aquatic and animal studies where sightlines for cameras and observers are the design driver, and interior surfaces must be cleanable without hazing.
- Flow-visualization channels — long, optically clean working sections where straightness and wall flatness matter, because the walls are effectively optical windows onto the flow.
- Media baths and process tanks — working vessels for wet processes where seeing level, contents, and condition at a glance is the point.
- Calibration chambers — vessels built around an instrument’s geometry, with penetrations placed exactly where the sensor package needs them.
Different studies, same fabrication spine: bonded transparent panels, machined penetrations, and a joint system asked to hold liquid for years while staying invisible.
Joint engineering for liquid service
A dry display case’s joints answer to the eye; a tank’s joints answer to water, permanently. The fabrication practices that difference drives:
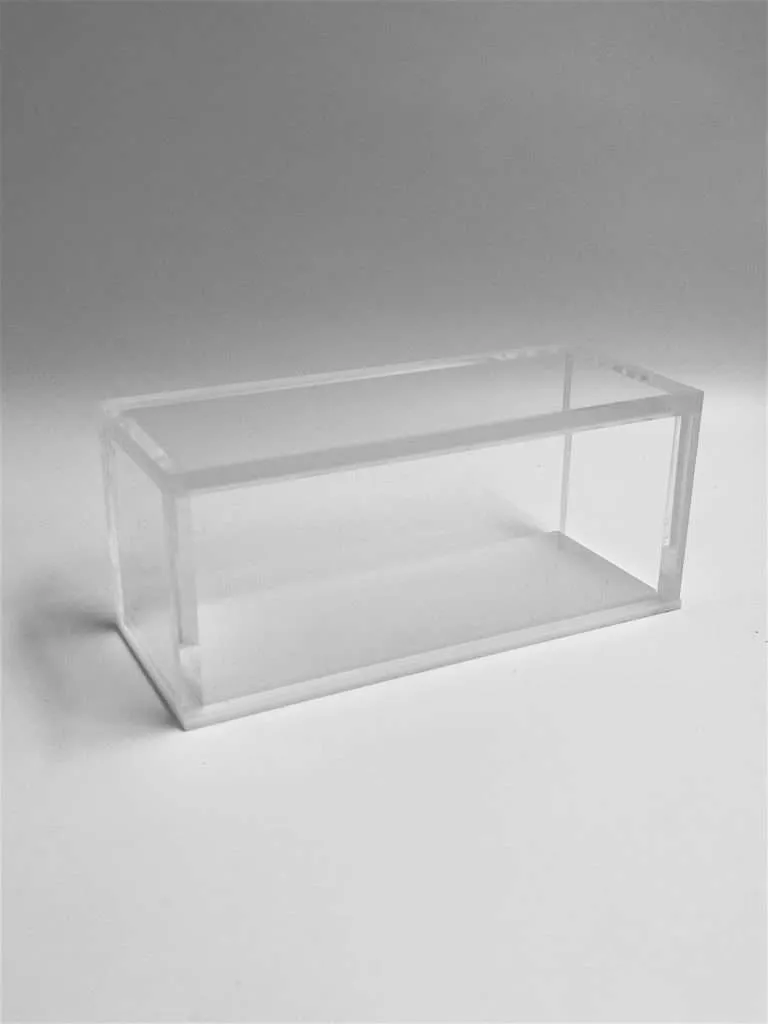
- Joint geometry. Chosen, not defaulted: a simple butt joint bonds face-to-edge; a rebated (stepped) joint registers the panels mechanically and increases the bonded area along the seam. Which geometry a tank gets depends on wall thickness and panel size — larger, deeper vessels earn the more interlocked joints.
- Adhesive system. It follows the section: thin-section work solvent-bonds — the joint is acrylic welded into acrylic. Larger sections and heavier walls move to two-part cement, which cures into a structural layer and fills the joint volume a big rebate presents. The choice is a fabrication-engineering call made per vessel, and it is one of the legitimate questions to ask any shop quoting tank work.
- Interior fillet beads. Liquid-service joints commonly carry a run of adhesive laid as a fillet along the interior seam — added bonded area and a smooth, cleanable interior corner where a sharp one would trap residue.
We build these tanks and chambers regularly — bonded, in the sizes and configurations above, with the joint engineering that liquid service asks for — and we build them to your specification: your wall thickness, your drawing, your protocol. What we do not typically issue is a pressure or containment rating; the vessel goes into service after your own fill test, filled per your protocol, held, and inspected, which is how research groups already commission equipment. Bring the spec and the study it serves, and the joint construction, features and stand get designed around it
Depth drives thickness — honestly
The load on a tank wall is hydrostatic: it grows with depth, which makes tank height the dimension that drives wall thickness, more than footprint. A long shallow channel and a compact deep column are opposite problems — the first is a flatness and straightness job, the second is a wall-section job.
Where the thickness number comes from is a responsibility question with a clean answer: from the customer’s specification, or from published tank-design guidance the customer selects — and the fabricator confirms buildability: that the specified sections can be machined, bonded, and assembled to the drawing. Research groups building serious vessels usually arrive with exactly this — a PI or facilities engineer has run the numbers, or the group is scaling a published design. What we add is the fabrication reality check: whether the joints the spec implies are the joints the geometry can actually carry, and where the design’s tolerances need to live per our Fabrication Tolerances standard.
Features that make a tank usable
The difference between a box that holds water and a research instrument is the feature list — all machinable, all vastly cheaper at fabrication than retrofit:
- Bulkhead-fitting penetrations — holes machined to the fitting manufacturer’s specified size, located to the drawing, with flat sealing lands. Drains, sensors, supply lines, and cable ports all live here; locating them precisely at CAD beats field-drilling a finished vessel in every possible way.
- Reinforced top flanges — a bonded perimeter flange stiffens the open rim of a topless tank (the structurally loneliest edge it has), doubles as a mounting land for lids and instrumentation bars, and gives handling a place to hold.
- Interior partitions and baffles — dividers and flow-conditioning elements bonded inside the vessel during fabrication, plumb and located, rather than improvised into a finished tank.
- Stands and secondary containment — the tank’s supporting structure, sized to the filled weight, is part of the same design conversation; water is heavy and benches vary.
Lifecycle honesty: aging, inspection, and the duplicate decision
Bonded tanks are working equipment, and working equipment ages. Years of fill cycles and cleaning chemistry act on the material and its joints — which is why mature lab programs put tank joints on the same casual inspection rotation as everything else with a service life: look along the seams for developing haze, whitening, or fine crack networks at the bonded corners, especially after any cleaning-chemistry change (aggressive cleaners are a classic stressor for acrylic — a compatibility-chart check before adopting a new protocol is cheap insurance).
And the decision experienced labs get right: when a veteran tank’s joints start showing age, the answer is usually duplication, not repair. The vessel exists as a drawing in the fabricator’s records; a new build from that drawing is a known-good instrument with a fresh service life, while a field-repaired joint is a patch on the oldest chemistry in the vessel. Plan the replacement while the original still works, on the ordinary schedule — in Production Scheduling terms, that is unhurried Production Schedule work, which is exactly the point of planning it early. When there’s a vessel on your bench that fits this description — or a drawing that needs to become one — send the drawing and the fill depth, and the buildability conversation starts from there.