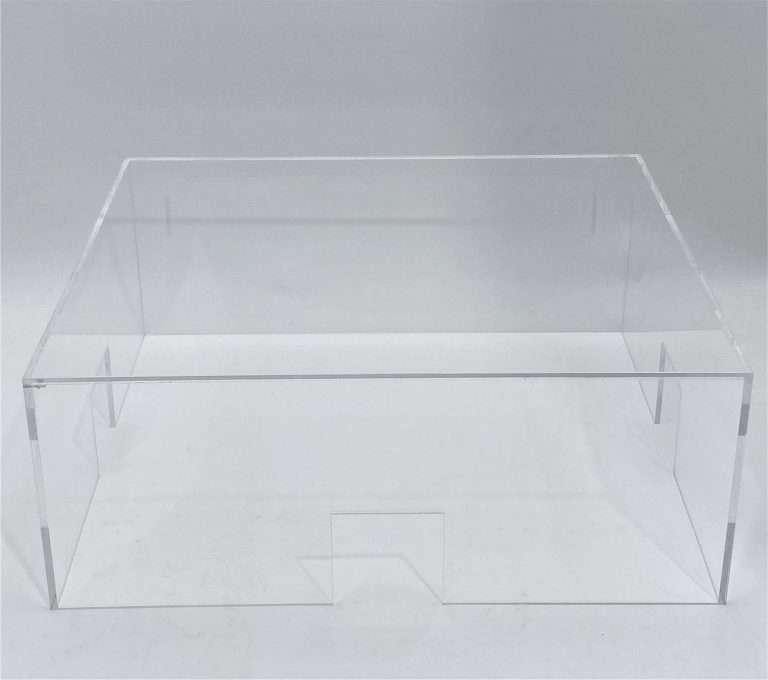
Aluminum extrusion made enclosure framing a catalog product, and the catalogs are good: standard bays, standard panel kits, standard hardware. Then the actual cell gets designed, and reality produces what catalogs can’t — a bay sized by the robot’s reach rather than by round numbers, a door panel with a handle and an interlock switch cutout, a pass-through with a conveyor-shaped hole in it, a notch where the cable track exits. Integrators and plant engineers building cells from T-slot framing end up needing custom clear infill on nearly every build, and the panels are easy to get right if the drawing respects how frame systems actually hold panels.
Panel size comes from the frame system, not the bay
The most common error in infill drawings is dimensioning the panel to the bay opening — or worse, to frame centerlines. A captured panel has to sit inside the slot with the engagement and clearance the frame system’s documentation specifies; a surface-mounted panel has to overlap the frame by the system’s stated margin. Every major extrusion system publishes its panel allowance for exactly this reason. Derive each panel dimension from that published allowance and the measured frame, and state the retention method on the drawing:
- Captured in slot — the panel edges live inside the extrusion slot. Edges are concealed, so they take an economical machine finish; what matters is the dimension, because a panel cut to the bay size simply will not go in.
- Surface-mounted with fasteners — the panel overlaps the frame face and bolts to it. Now the hole pattern is the critical feature, and holes in plastic want to be oversized for movement, per the sheet manufacturer’s published fabrication guidance — slotted holes on long panels are the standard move, and clear plastics move more with temperature than the aluminum they’re bolted to (the mechanism and the design response are covered in thermal expansion and clearance).
Either way, the drawing that quotes cleanly carries: the frame system and slot series, the retention method, panel dimensions derived from the allowance, and which edges (if any) are exposed. Everything else runs on the published Fabrication Tolerances.
Material: usually polycarbonate, cut the right way
Most cell infill is guarding, and the guarding logic applies: where the process can throw a part or a tool, polycarbonate is the usual call, with acrylic earning its place on faces where impact isn’t the exposure and clarity or scratch behavior matters more — the full decision is in polycarbonate vs acrylic for machine guarding, and what the relevant OSHA language actually asks of guard material is unpacked in our read of 1910.212. One process note that surprises people specifying polycarbonate: it is not laser-cut — polycarbonate panels are cut by saw and CNC, which handles every cutout on a cell panel (and holds the tolerances that matter) without the laser. If a drawing note says “laser cut” on a polycarbonate part, the note needs to change, not the material.
Doors, pass-throughs and the interlock line
Door panels are where cells get custom fastest: hinge hole patterns, handle cutouts, and the rectangular cutout for the interlock switch body. All of it is ordinary CNC work when it is located on the drawing — located, specifically, to the controls drawing, because the interlock’s position belongs to the integrator’s safety architecture. That is the scope line worth stating plainly: the integrator owns interlock logic, guard openings, and the cell’s safety design; the fabricator’s job is panels cut precisely to that design. Where something on a panel drawing looks off — a cutout that lands on a slot line, a hole pattern that can’t clear the hardware — we flag it and the design call goes back to the people who own the cell.
Repeat cells: the second one should be a reorder
Cell designs repeat — a line gets duplicated, a second plant wants the same cell, panel seven gets forklifted. When a cell’s panel set exists as a dimensioned, numbered record, the next set is a release rather than a re-measuring exercise: for programs built to repeat we keep the fuller record (drawings, setups, notes), which is what makes panel seven, ordered alone two years later, match the one it replaces. How that record works is covered in reorders and files on record, and the ordering pattern for OEMs building cells on a cadence is in the contract manufacturing guide.
To get a panel set quoted: the frame system and series, the panel schedule (or the frame drawing to derive one), retention method per panel, material and thickness, and the cutout drawings for doors and pass-throughs — through the RFQ form. The broader discipline of drawing plastic parts that quote and build cleanly is the design for fabrication guide‘s whole subject; cell infill is just that discipline applied to a frame someone else already engineered.